Egg grading, counting and line efficiency with cameras: 18 lines in one system, 0.69% errorAt an egg facility, existing cameras count eggs and classify them as large/small; 18 collection lines merged into one system, with a measured error rate of 0.69%.2025-01-02
At an egg (poultry) production facility, eggs came from 18 separate collection lines and merged onto a single conveyor toward grading and packing. Counting the eggs and sorting them by size was largely manual and based on estimates. Hype Vision connected the facility's existing cameras to AI: a system that counts eggs one by one, classifies them as large/small and measures line efficiency. The error rate measured on site was 0.69%.
The problem: 18 lines, manual counting and sizing
Eggs came from 18 different collection lines and merged onto one conveyor. In this dense flow, counting eggs accurately and sorting them by size was almost impossible by hand; counting relied on estimates and line efficiency could not be measured.
Rather than installing new, expensive optical grading lines, the facility wanted to use its existing cameras.
18 lines into one: egg counting
Eggs arriving from 18 collection lines and merging onto one conveyor are detected one by one by the existing camera, each tracked with its own ID; an egg crossing the defined counting line is counted, and the same egg is not counted twice. Total and time-based output appears on the dashboard in real time.
- One-by-one egg counting on the merged line
- Each egg a separate ID — no double counting
- Accurate crossing count with a counting line
- Real-time, timestamped production quantity
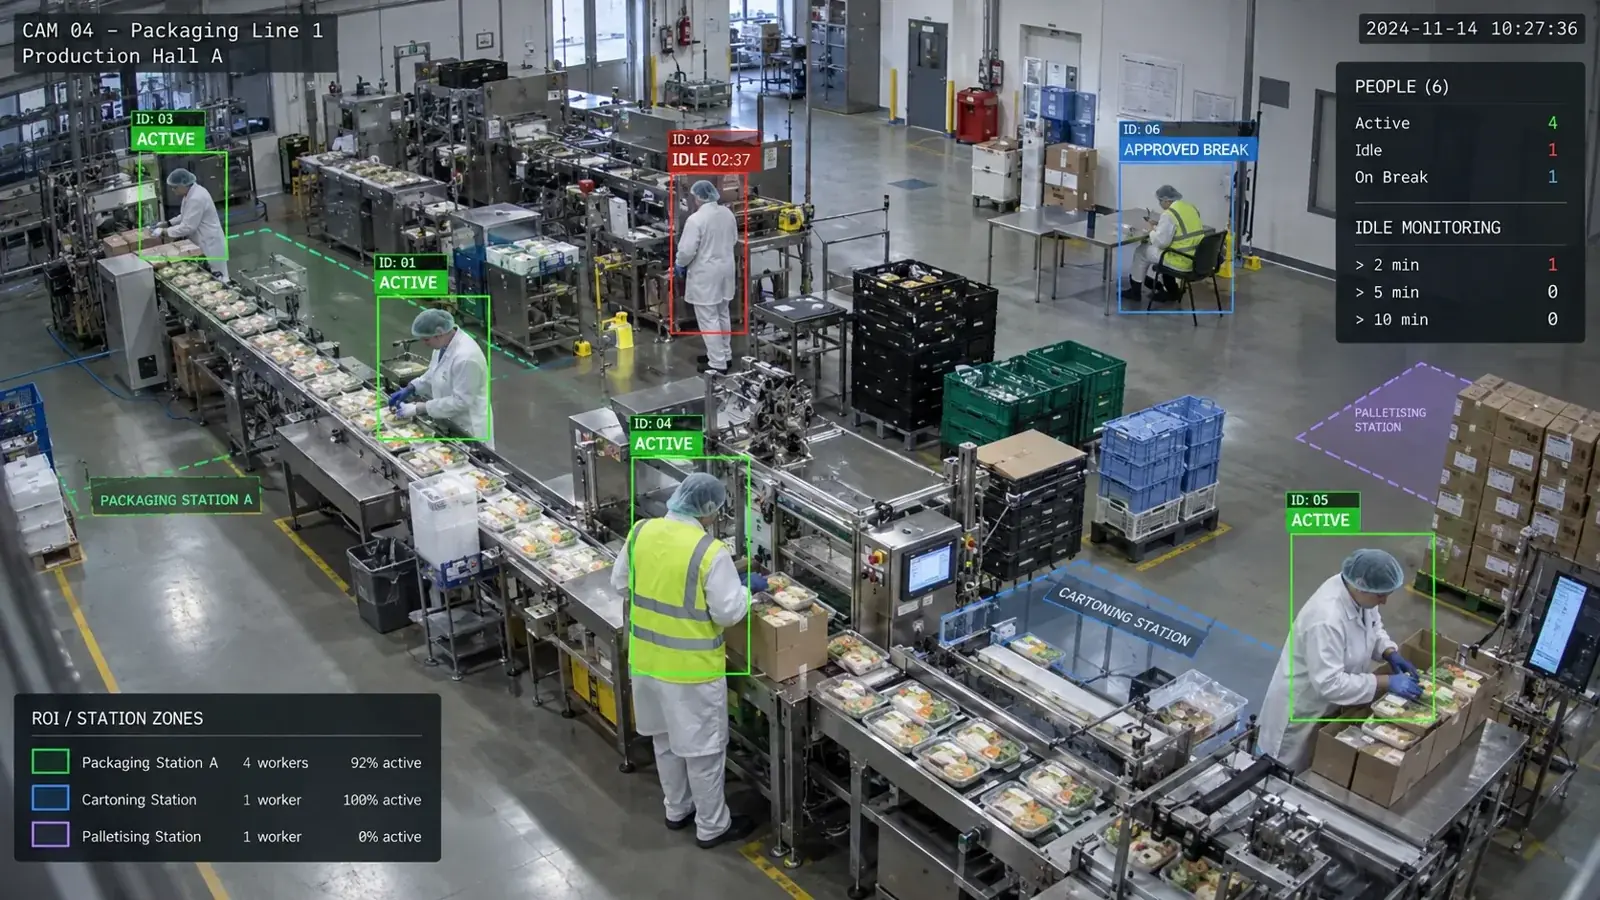
Egg classification: large / small
During counting, eggs are classified by size: large and small eggs are marked separately (e.g. large in green, small in orange). So not only the total count but also the size distribution is visible in real time, and production and packing are planned with data.
- Size classification (large / small)
- Real-time visibility of size distribution
- Sizing data together with the count
- With existing cameras — no extra optical line needed
Line efficiency and accuracy
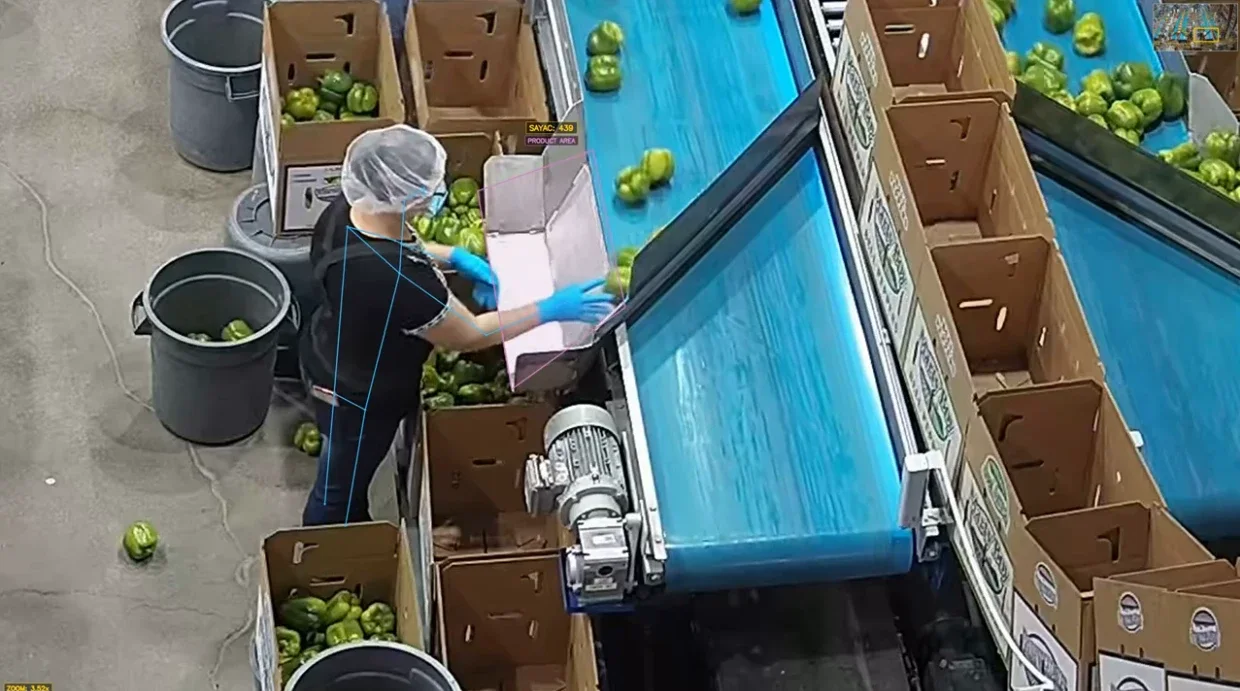
The same system also measures line efficiency: production speed, active/idle times and the combined output of the 18 lines are tracked. The error rate measured on site was 0.69%, meaning counting and classification were done continuously and with high accuracy compared with manual checking.
The setup used the facility's existing cameras, not a new grading machine.
- Production speed and active/idle time
- Combined output of the 18 lines tracked
- 0.69% error rate measured on site
- With existing cameras, no extra hardware investment
Facility and setup
Eggs are carried from the barn to the packing area by collection lines; the camera is positioned to see the conveyor where the lines merge. Analysis runs on-premise, video does not leave the site; results are collected on the dashboard and can be pushed to an ERP/packing system if wanted.
Outcome
Egg counting and sizing moved from manual and estimate-based to continuous, automatic and high-accuracy. The combined output of 18 lines is tracked in one system, with large/small sorting and a 0.69% error rate — all with existing cameras.
- 18 lines merged into one system
- Egg counting + large/small classification
- 0.69% error rate measured on site
- Existing cameras, no extra optical line
Frequently asked questions
Do I need a new optical grading machine?
No. This setup used the facility's existing cameras; eggs were counted and classified as large/small from the camera. There was no need to install an expensive optical grading line.
What is the error rate?
The error rate measured on this site was 0.69%. Accuracy varies with camera angle, lighting, conveyor speed and egg flow density, and is verified on site during the pilot.
How do you merge 18 lines into one system?
Because the 18 collection lines merge onto one conveyor, the camera at the merge point sees the whole flow; eggs are counted and classified there one by one. Per-line counting can also be configured if needed.
Does video leave the facility?
No. The deployment is on-premise; analysis runs on a server inside the facility and only count, class and metric data reach the dashboard.