AI visual quality inspection for production linesAI-based visual inspection for surface defects, assembly errors, labels and print. Camera and lighting assessment, custom model training, validation and line integration.
Inspect every unit at line speed for visible defects — and keep an image record of each decision.
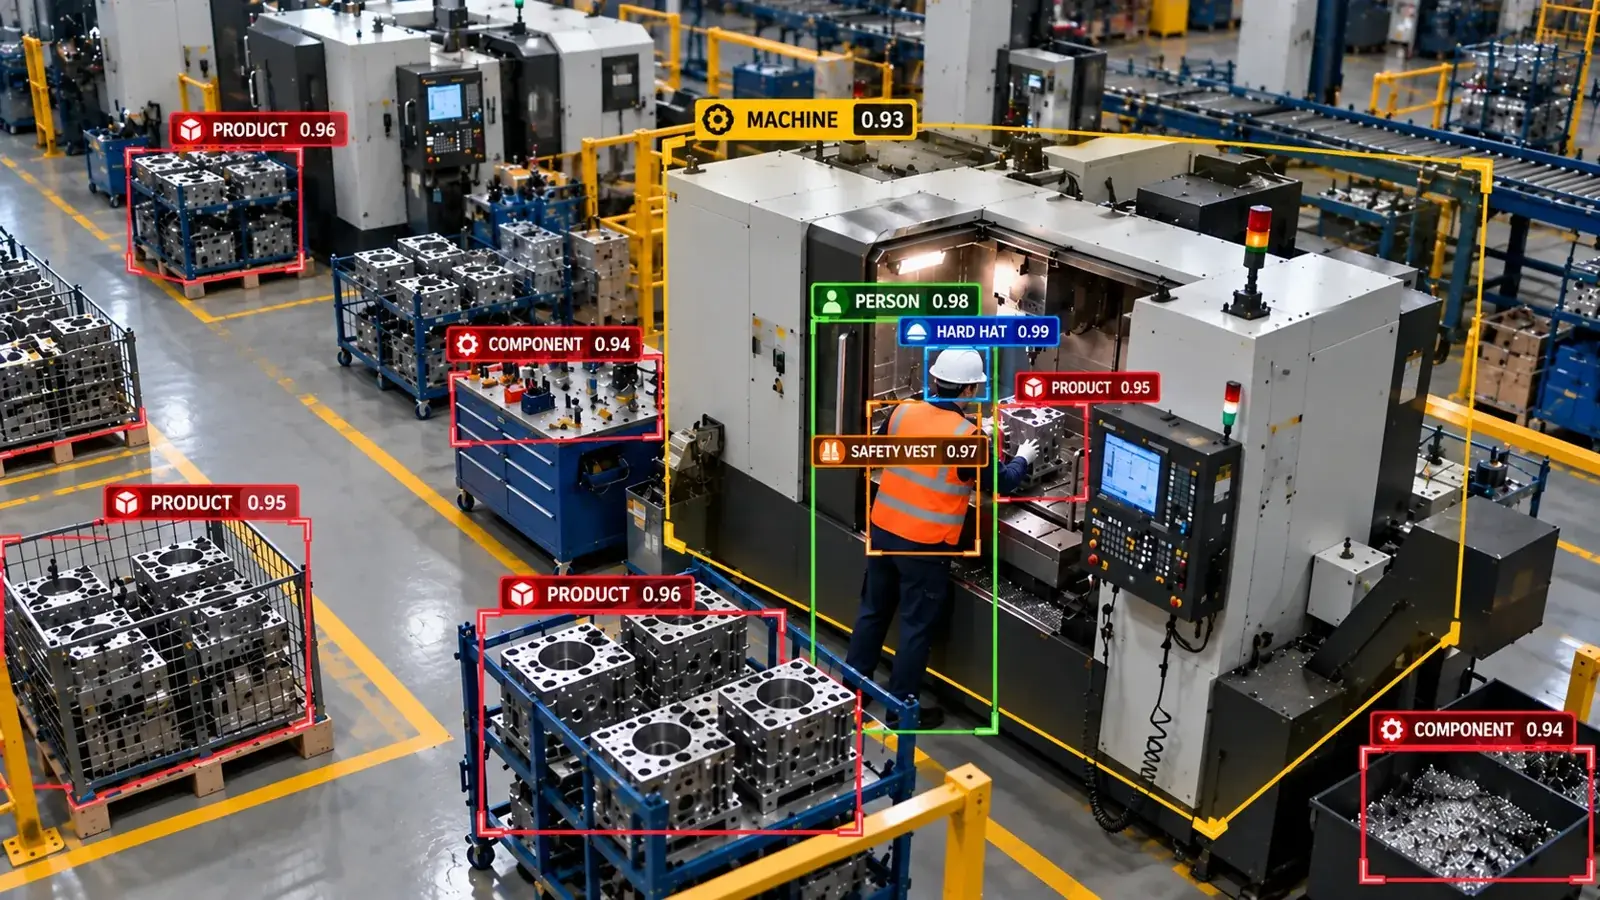
AI visual quality inspection uses cameras and deep-learning models to detect visible defects such as scratches, dents, missing components or wrong labels on products, and to classify units as OK or not OK.
The problem
Manual visual inspection is sampled, tiring and inconsistent between shifts. Escaped defects lead to customer complaints and returns; over-rejection creates unnecessary scrap.
Rule-based machine vision works well for fixed, repeatable checks but struggles with natural variation in materials, lighting and product variants.
How it works
Existing IP cameras / NVR
RTSP / ONVIF streams
Edge device on-site
AI models + rules; video stays local
Events
Time, camera, zone, evidence frame
Dashboard, alerts, API
Notifications, relays, REST/webhook
- 1 Defect types are defined with your quality team and sample images are collected.
- 2 Camera position, optics and lighting are selected for the smallest defect that matters.
- 3 A model is trained and validated on images it has not seen before.
- 4 Results are connected to the line: reject signals, operator alerts and records in MES/ERP.
What can be detected
- Surface defects (scratches, dents, stains, cracks)
- Assembly errors (missing or misplaced parts)
- Label and print errors
- Defect trends by line, product and shift
Typical scenarios
- End-of-line inspection
- In-process inspection after critical steps
- Incoming goods inspection
- High-variation products such as textiles, castings or natural materials
Deployment options
On-premise / edge
Analysis runs on hardware inside your network. Video does not leave the site; only events and metrics are stored or shared.
Cloud
Suitable for distributed, low-camera-count sites where central management matters more than keeping video on-site.
Hybrid
Video is processed on-site, while events, dashboards and multi-site reporting are managed centrally.
Working with existing cameras
- Unlike safety use cases, inspection often needs dedicated industrial cameras and controlled lighting.
- The required resolution follows from the smallest defect size and the field of view.
- Most IP cameras and NVRs that provide RTSP or ONVIF streams can be connected, regardless of brand.
- Before a pilot, sample footage from each candidate camera is reviewed for resolution, angle, distance and lighting.
- Where a view is not suitable, the recommendation is usually to reposition the camera or add one — not to replace the whole system.
Integration
- PLC signals for rejection
- REST API to MES/ERP
- Image archive for traceability
Privacy and security
- No face recognition is used in safety and operations analytics; events describe what happened, not who.
- On-premise processing keeps video inside your network.
- Evidence clips, retention periods and user access are configurable and should follow your GDPR/KVKK policies.
- Workplace monitoring should be introduced with clear employee information and, where applicable, consultation with employee representatives.
Limitations
- Defects that are not visible to the camera (internal, behind surfaces) cannot be detected.
- Rare defects may need anomaly-detection approaches and more validation time.
- Escape and false-reject rates are measured separately; both matter.
How a pilot works
Frequently asked questions
It depends on the defect type and variation. Common defects may need hundreds of examples; for rare defects, anomaly detection trained on good parts is often used.
Line speed is measured during discovery and camera, triggering and edge hardware are chosen accordingly.
Related solutions
Industries
Case studies
Further reading
Start with the cameras you already have
Send us a few frames from your cameras and the problem you want to solve. We will tell you honestly what is feasible.
Related case studies
Frequently asked questions
How many defect images do we need?
It depends on the defect type and variation. Common defects may need hundreds of examples; for rare defects, anomaly detection trained on good parts is often used.
Can it keep up with our line speed?
Line speed is measured during discovery and camera, triggering and edge hardware are chosen accordingly.
What can AI detect in your factory?
Let's review together which safety, quality and production analytics your existing security cameras can deliver.
- Free 15-minute technical call
- Camera infrastructure pre-assessment
- Feasible AI scenarios