Industrial Computer Vision for Factories & PlantsIndustrial computer vision adds AI video analytics to the CCTV you already have: PPE, forklift–pedestrian, quality and OEE. Edge/on-premise, brand-agnostic. Free pre-assessment.
A practical guide for HSE, operations and plant managers: what computer vision can do in industrial sites, what it needs, and how to start without replacing your camera system.
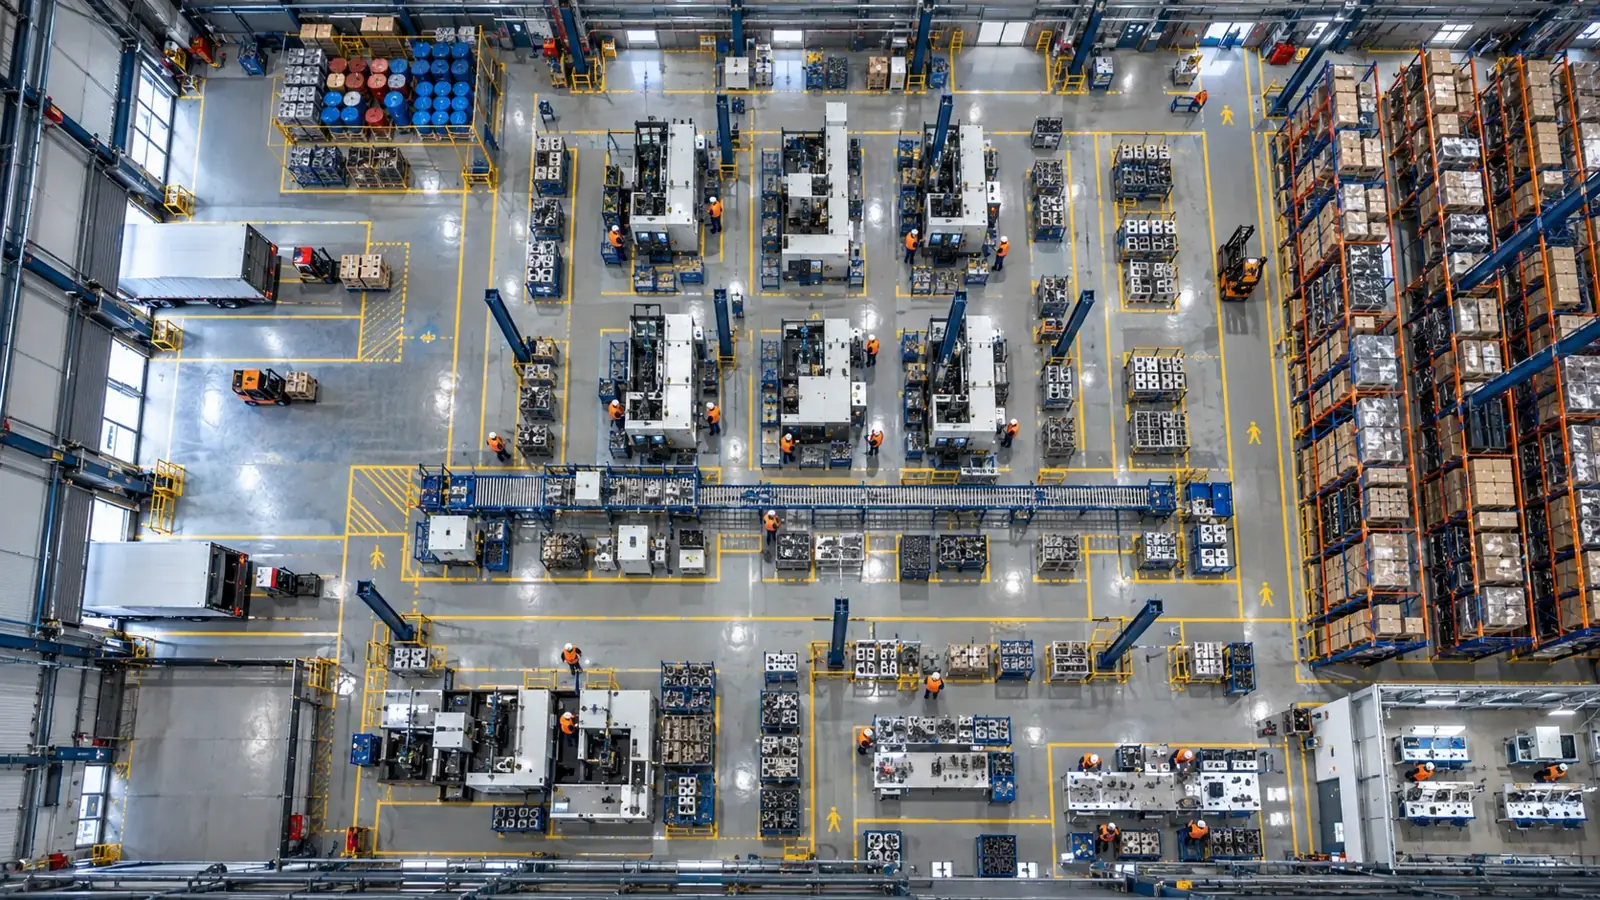
Industrial computer vision is the use of cameras and AI models to automatically detect, measure and classify what happens in factories, warehouses and other operational sites — for example PPE compliance, people in danger zones, line stops, product counts or visible defects — and turn it into alerts and data.
Solutions
Existing IP cameras / NVR
RTSP / ONVIF streams
Edge device on-site
AI models + rules; video stays local
Events
Time, camera, zone, evidence frame
Dashboard, alerts, API
Notifications, relays, REST/webhook
How is existing CCTV used for AI analytics?
Most industrial sites already have IP cameras recording to an NVR or VMS for security. Those cameras expose video streams (typically via RTSP , often discoverable via ONVIF ). An analytics system reads the stream, runs detection models on each frame, applies rules (zones, schedules, durations) and outputs events. The cameras and recording system stay as they are.
Not every view is suitable for every use case. A camera that is fine for detecting a person in a restricted zone may be too far away to check safety glasses. That is why camera assessment comes before any commitment — see how to evaluate cameras for computer vision .
Edge vs on-premise vs cloud
For most industrial projects, on-premise processing is the default because it keeps video inside the network and works with limited internet bandwidth. More detail: edge vs cloud video analytics .
| Edge / on-premise | Cloud | Hybrid | |
|---|---|---|---|
| Where video is processed | On hardware inside the site network | In a cloud environment | On-site |
| Video leaves the site | No | Yes | No (events only) |
| Bandwidth need | Low | High (continuous upload) | Low |
| Typical fit | Plants, banks, sensitive sites | Small, distributed sites | Multi-site organisations |
Typical manufacturing use cases
Workplace safety
PPE detection , restricted area monitoring , forklift–pedestrian detection , fall detection and fire and smoke detection give HSE teams continuous coverage instead of periodic walk-arounds.
Quality inspection
Visual quality inspection detects visible defects at line speed. Unlike safety use cases, it usually needs dedicated cameras and lighting at the inspection point.
Production and operational analytics
Production line monitoring , product counting and workstation analytics measure running time, micro-stops, output and bottlenecks — including on older machines without PLC data.
Camera requirements
- Stream access: RTSP/ONVIF from the camera or NVR.
- Resolution and distance: the subject must cover enough pixels; 1080p is usually enough for people-level events at moderate distance.
- Angle: angled views from above work better than strict top-down views for PPE and posture.
- Lighting: stable lighting or good IR for night operation; strong backlight is a common problem.
- Frame rate: fast processes (vehicles, conveyors) need higher frame rates.
Deployment process and integration
A typical project moves from discovery and camera assessment to a defined pilot, validation on your own footage, and a rollout decision. Events are delivered to a dashboard and notifications, and can be sent to other systems via REST API/webhooks or local relay outputs. See how a pilot works .
Privacy
Industrial safety and operations analytics do not need to identify people. Hype Vision does not use face recognition for these use cases. With on-premise processing, video stays inside your network, and retention and access rules follow your GDPR/KVKK policies.
Limitations worth knowing
- Computer vision only sees what the camera sees; occlusion, distance and lighting set the limits.
- Camera-based monitoring is not a substitute for safety-rated machine guarding or certified fire detection.
- Performance varies per camera and must be measured on site, not quoted from a datasheet.
Where Hype Vision fits
Hype Vision develops computer-vision and AI video-analytics solutions that run on existing IP/CCTV cameras for industrial safety, manufacturing, quality and operational monitoring. The team is based at Bilişim Vadisi in Gebze, Türkiye, and has been working on industrial AI projects since 2020.
Not sure whether your cameras are suitable? Send a few frames and the problem you want to solve.
Frequently asked questions
Machine vision traditionally refers to rule-based inspection systems with dedicated industrial cameras and controlled lighting. Computer vision is the broader field; in industry today it usually means deep-learning models that also work on general CCTV footage and in variable conditions.
For on-premise processing, an edge device with suitable acceleration is used. The hardware is sized to the number of cameras and analytics during discovery.
It depends on the use case and number of cameras. Ready-made safety analytics can be deployed quickly; custom quality inspection models need time for data collection and validation.
In most projects, yes. Cameras or NVRs that provide RTSP or ONVIF streams can be connected regardless of brand. Each camera’s view is checked for suitability before a pilot.
Usually not for safety and operations use cases. Some views may need repositioning or an additional camera. Visual quality inspection often needs dedicated cameras and lighting.
Yes. Analysis can run on edge hardware inside your network so that video is processed locally.
Yes. In an on-premise deployment, video stays on-site; only event data and, if enabled, short evidence clips are stored for review.
Further reading
Start with the cameras you already have
Send us a few frames from your cameras and the problem you want to solve. We will tell you honestly what is feasible.
Related case studies
Frequently asked questions
What is the difference between machine vision and computer vision?
Machine vision traditionally refers to rule-based inspection systems with dedicated industrial cameras and controlled lighting. Computer vision is the broader field; in industry today it usually means deep-learning models that also work on general CCTV footage and in variable conditions.
Do we need GPUs on site?
For on-premise processing, an edge device with suitable acceleration is used. The hardware is sized to the number of cameras and analytics during discovery.
How long does a pilot take?
It depends on the use case and number of cameras. Ready-made safety analytics can be deployed quickly; custom quality inspection models need time for data collection and validation.
Can Hype Vision work with existing CCTV cameras?
In most projects, yes. Cameras or NVRs that provide RTSP or ONVIF streams can be connected regardless of brand. Each camera’s view is checked for suitability before a pilot.
Do we need to replace our cameras?
Usually not for safety and operations use cases. Some views may need repositioning or an additional camera. Visual quality inspection often needs dedicated cameras and lighting.
Can the system run on-premise?
Yes. Analysis can run on edge hardware inside your network so that video is processed locally.
Can it operate without sending video to the cloud?
Yes. In an on-premise deployment, video stays on-site; only event data and, if enabled, short evidence clips are stored for review.
What can AI detect in your factory?
Let's review together which safety, quality and production analytics your existing security cameras can deliver.
- Free 15-minute technical call
- Camera infrastructure pre-assessment
- Feasible AI scenarios